AI Summary
Running multi tier mezzanines well depends on how work moves between levels, not only on the steel structure. Warehouse teams must allocate products by demand and handling needs, set picking and replenishment routes that avoid conflict, locate transfer areas and temporary holding zones, and provide adequate lighting and practical staff access on every level. Agreeing these decisions before layout approval helps planners brief their mezzanine supplier with clear operational requirements and confirmed project boundaries.
Why Multi Tier Mezzanines Need an Operating Plan
A warehouse mezzanine floor adds space, but each extra level also adds travel paths, replenishment duties and points where orders change hands. Multi tier mezzanines therefore need an operating plan as detailed as the structural drawings.
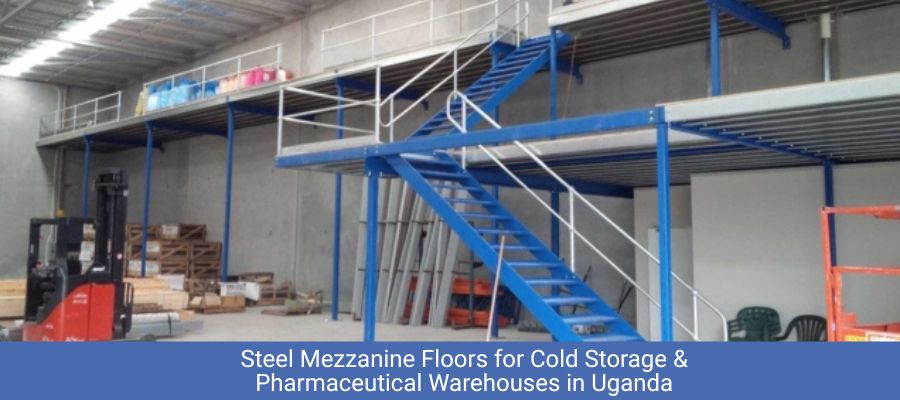
Build Matt fabricates steel mezzanine floors and mezzanine platforms, including multi tier configurations, for warehouses across Uganda and East Africa. This article covers the operational decisions to settle before sharing a brief with Build Matt.
Multi Tier Mezzanines: Allocating Products to Each Level
Product placement should follow operational data rather than habit. Before assigning stock to a level, review the following for each item or product family:
- Picking frequency and order line demand over a representative period.
- Item dimensions, weight and any special handling needs.
- Products that regularly appear on the same orders.
- Replenishment frequency and where reserve stock is held.
- Seasonal peaks and expected changes to the product range.
- Whether the available handling method can serve that level.
In mezzanine systems serving mixed order profiles, placing every fast moving item on the ground floor is not automatically best. Concentrating high demand lines can cause congestion, and splitting items often ordered together adds consolidation work. A spare parts distributor, for example, may keep small, frequently picked components in upper level shelving while bulky cartons stay near dispatch.
Operational slotting is separate from structural approval. Heavy stock and concentrated loads must stay within the approved design, so Build Matt should receive the intended storage arrangement for each level before load requirements are fixed.
Mezzanine Systems for Coordinating Picking and Replenishment
When stock arrives on a level while staff are picking, both activities may need the same working space. Written workflow rules give staff a consistent way to manage shared aisles, equipment and pick faces.
- Separate replenishment routes, or fixed time windows where separate routes are impractical.
- A priority rule for when picking and replenishment need the same aisle.
- Replenishment triggers based on expected demand and available stock, not only empty locations.
- Pick face quantities sized to last between scheduled replenishment cycles.
- A defined method for urgent shortages, including who authorises an unscheduled movement.
- Named responsibility for requesting, moving and confirming each replenishment.
The picking method shapes these rules. Discrete picking handles one order at a time, zone picking assigns staff to defined areas, and batch picking combines picks for several orders into one trip. A zone may cover part of a level or an entire level, depending on travel distances, workload and transfer arrangements. No method suits every operation, so test each option against your own order profile.
Mezzanine Platforms: Planning Transfer Points and Temporary Holding Areas
For each transfer point, estimate the number of totes, cartons or pallets expected during the busiest operating period. Compare that demand with the equipment’s usable capacity, including loading, unloading and waiting time. Use the resulting queue estimate to plan temporary holding space, with its permitted loading confirmed in the structural design.
- Locations for approved goods lifts, conveyors or other specified transfer equipment.
- Separation of inbound replenishment from outgoing picked orders where volumes justify it.
- Clear marking of goods awaiting movement, collection or checking.
- Defined handover responsibility between the sending and receiving level.
- Transfer queues kept clear of stairs, pedestrian routes and exits.
Equipment for moving goods must be distinguished from equipment approved to carry people, and a goods lift or conveyor should never become an informal staff route. Transfer equipment, loading gates and edge protection need appropriate specialist design. Build Matt supplies loading gates within its mezzanine access systems, so confirm early which interfaces fall within Build Matt’s scope.
Warehouse Mezzanine Floor Lighting, Visibility and Staff Movement
Decks, shelving and stored goods all block light, so working conditions on a lower tier can differ sharply from the level above. Review each level against these points:
- Task lighting at picking faces and label reading positions.
- Shadows cast by decks, shelving and stored goods.
- Sight lines at aisle intersections and transfer points.
- Consistent identification of levels, aisles and locations.
- Stair positions relative to normal staff journeys.
- Separation of pedestrian movement from goods handling.
- Emergency routes coordinated with the relevant building and fire requirements.
Stair positions should be checked against normal staff journeys so routine movement follows the planned access routes. Lighting levels, aisle widths, stair dimensions and exit numbers depend on the building and applicable regulations. Build Matt fabricates staircases and guardrails for its mezzanines, so share planned staff routes when agreeing access positions.
Multi Tier Mezzanines and Order Consolidation Across Levels
When an order contains items from several levels, those picks must come together as one complete, checked order. Without a defined control, partial orders can reach packing unnoticed.
- Clear identification of each order, tote or container.
- Confirmation from each level that its assigned picks are complete.
- A defined consolidation location.
- A process for missing, damaged or incorrectly picked items.
- A rule that stops incomplete orders moving to packing or dispatch.
- Visible order status through a suitable manual or digital process.
The control matters more than the tool. A status board, paper pick list or warehouse management system can all work if every level follows the same confirmation steps.
Warehouse Mezzanine Planning Checks Before Layout Approval
Use this table to confirm each operational decision has supporting evidence before the layout is approved, then walk through a representative busy period. Trace expected orders and replenishment movements level by level, and treat each unresolved conflict as a decision to settle before fabrication.
| Planning check | Evidence to review |
|---|---|
| Product allocation | Demand data, item dimensions and handling needs by level |
| Picking and replenishment interaction | Agreed routes, time windows and priority rules |
| Transfer throughput | Peak demand compared with usable equipment capacity |
| Temporary holding boundaries | Marked areas sized to the queue estimate |
| Staff routes and visibility | Drawings showing stairs, crossings and lighting positions |
| Order consolidation | Named responsibilities and confirmation steps |
| Structural and building constraints | Load, access and fire requirements confirmed by responsible specialists |
About Build Matt and Steel Mezzanine Floors
Build Matt, established in 2001 in Kampala’s Industrial Area, manufactures pre engineered buildings and fabricates steel structures for clients in Uganda, South Sudan, Rwanda, Burundi, the Democratic Republic of Congo and Kenya. Its steel mezzanine floors include multi tier configurations, staircases, guardrails and loading gates, supported by site measurements and load evaluations. Sharing storage arrangements, equipment interfaces and operating requirements helps Build Matt confirm the project scope accurately.
Planning Multi Tier Mezzanines Around Daily Operations
Planning how stock, people and orders move between levels helps align multi tier mezzanines with daily operations. Those decisions shape load zones, stair positions and access points. Warehouse teams planning a new or expanded mezzanine can share their operating requirements with Build Matt to discuss the right project scope.
Multi Tier Mezzanines Planning FAQs
What information should a warehouse brief include before mezzanine floor fabrication?
Include the intended stock and storage equipment for each level, expected loads, handling equipment, transfer points, and planned stair and gate positions. Note any interfaces with lifts or conveyors. A complete brief helps Build Matt confirm the fabrication scope and identify items needing other specialists.
How can picking and replenishment avoid competing for the same space?
Agree in advance which activity takes priority in a shared aisle, and schedule routine replenishment around known picking peaks. Review the rule after the first busy periods of operation, because actual order patterns may differ from planning forecasts.
Where should transfer points be located on mezzanine platforms?
Locate them near the zones generating most transfers, with clear approach space on both levels. Confirm with Build Matt which loading gates and edge interfaces it will supply, and which transfer equipment needs a separate specialist supplier.
How should returns and damaged stock move between levels?
Give returns and damaged goods their own marked holding location and route, separate from saleable stock and picked orders. Decide who inspects each item, where it is assessed and which level receives restocked goods, so unchecked items stay away from active pick faces.
What happens when one level finishes its picks before another?
Completed picks wait in the consolidation area under the order’s identification until the remaining levels confirm. Set a maximum waiting time and an escalation step for a level that falls behind, so partial orders do not accumulate and block consolidation space.
How should seasonal demand changes affect product allocation?
Review allocation before each known peak rather than once a year. Moving seasonal lines temporarily can relieve busy zones, but heavy or dense stock must stay within each level’s approved load, as agreed with Build Matt at the design stage.
Founder & CEO
Mukesh Patel is the Founder & CEO of Build Matt ltd, specializing in Pre-Engineered Buildings (PEB) and general steel fabrication. With advanced technology, modern machinery, and a skilled workforce, he delivers efficient and high-quality solutions across East and Central Africa, including Uganda, Kenya, Tanzania, Congo, South Sudan, Rwanda, and Burundi.